


Solvent Recovery and Recycling: Industrial Guide
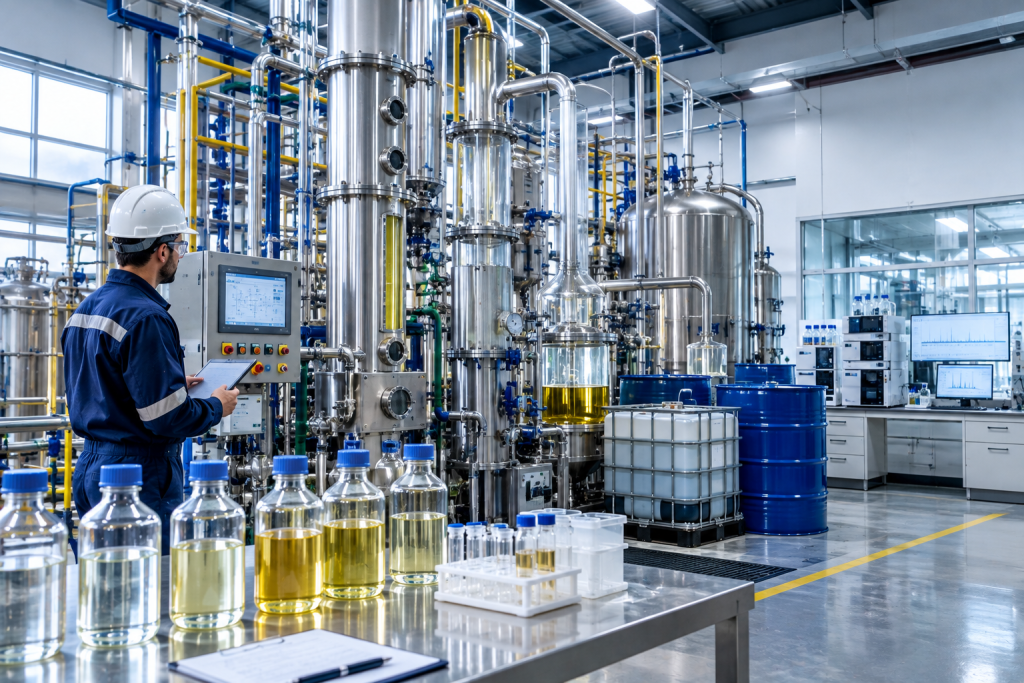
Solvent Recovery and Recycling helps industrial manufacturers recover usable solvents from selected process streams, reduce solvent waste and improve raw-material efficiency. Depending on solvent composition and required purity, recovery may involve distillation, condensation, adsorption, filtration or a combination of separation technologies. For chemical manufacturers, pharmaceutical producers, coatings companies and industrial cleaning operations, Solvent Recovery and […]
Pharmaceutical Solvents: Uses and Selection
Pharmaceutical Solvents: Applications and Selection Pharmaceutical solvents play a vital role in drug manufacturing, active pharmaceutical ingredient (API) production, extraction, purification, crystallization, and equipment cleaning. Selecting suitable solvents helps pharmaceutical manufacturers maintain process consistency, control impurities, and meet the quality requirements of their intended applications. Common pharmaceutical solvents include ethanol, isopropyl alcohol, acetone, and ethyl […]
Ethyl Acetate Uses: Industrial Applications
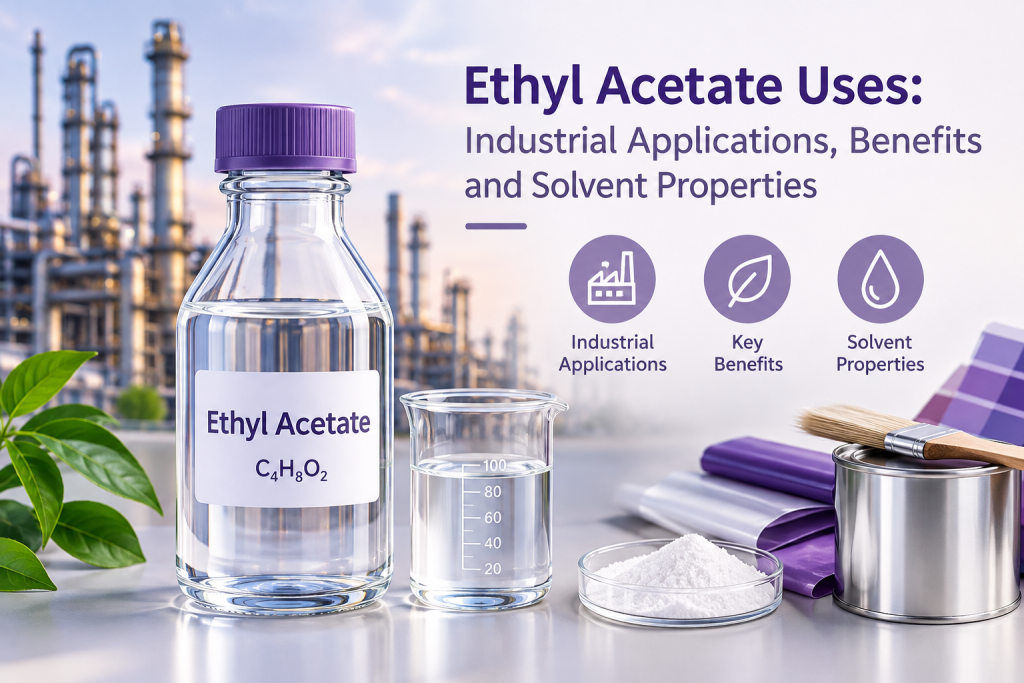
Ethyl Acetate Uses: Industrial Applications Ethyl Acetate Uses include paints and coatings, adhesives, printing inks, pharmaceutical processing, and selected food and cosmetic applications. Ethyl acetate is a volatile organic ester solvent valued for its ability to dissolve many resins and organic compounds and for its relatively rapid evaporation. With the chemical formula C₄H₈O₂ and CAS […]
Xylene Uses: Industrial Applications and Benefits
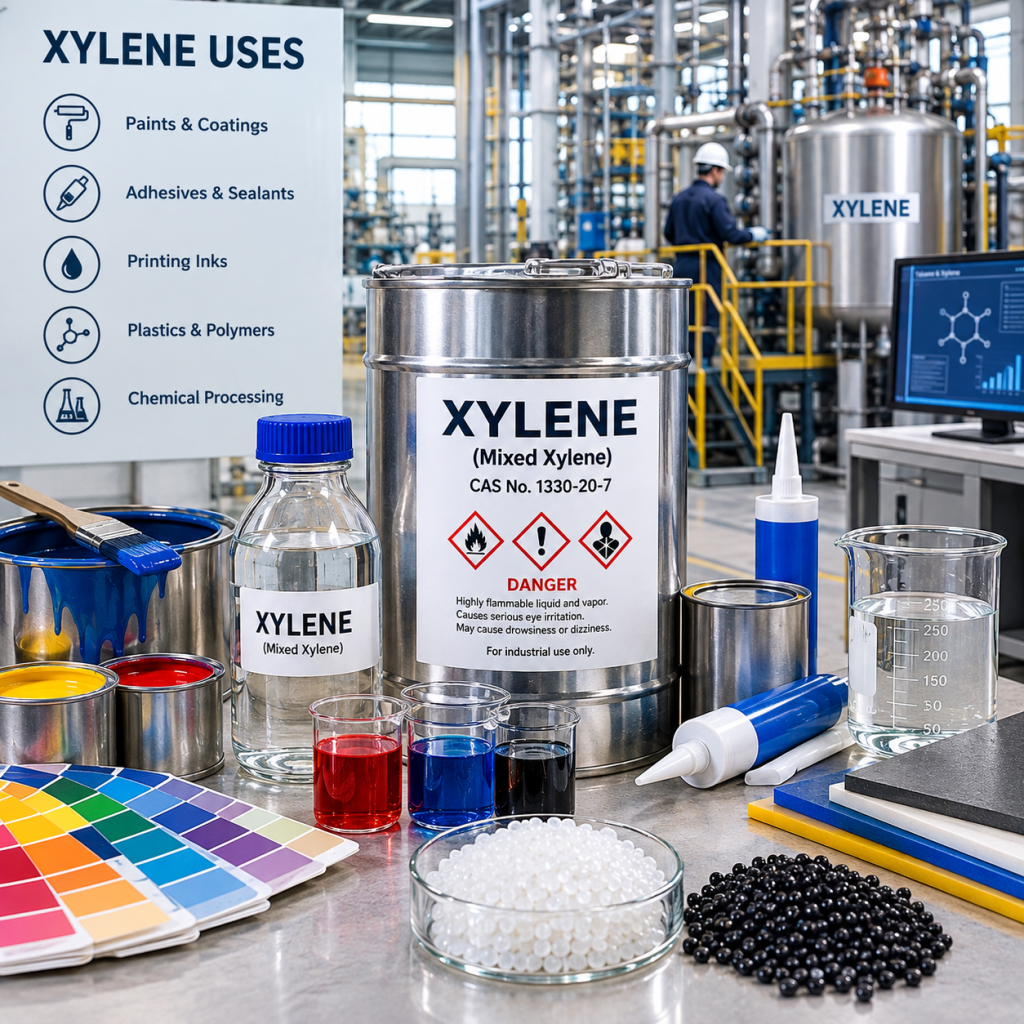
Xylene Uses: Industrial Applications and Benefits Xylene Uses include industrial solvent applications and petrochemical manufacturing. Xylene is an aromatic hydrocarbon available as three isomers—ortho-xylene, meta-xylene, and para-xylene—as well as commercial mixtures known as mixed xylene. Manufacturers use the appropriate grade according to its solvency, isomer composition, purity, and process requirements. From paints and coatings to […]
Methyl Ethyl Ketone Uses: Industrial Applications
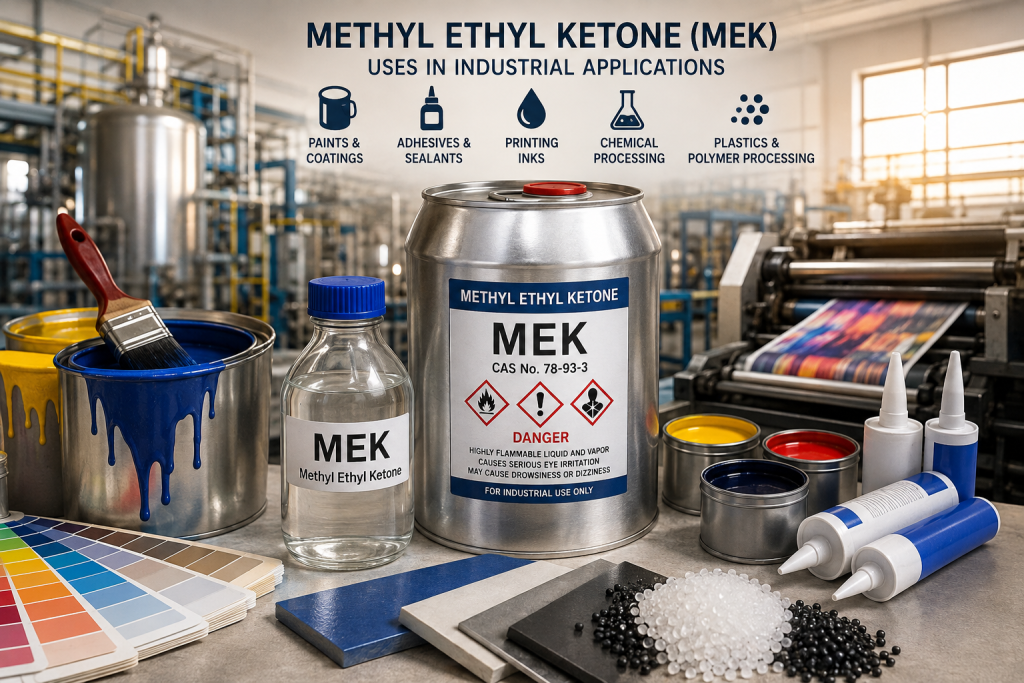
Methyl Ethyl Ketone Uses: Industrial Applications Methyl Ethyl Ketone Uses include solvent applications in paints, coatings, adhesives, printing inks, and selected industrial cleaning processes. Also called MEK or 2-butanone, methyl ethyl ketone is a volatile organic solvent valued for its strong solvency, relatively rapid evaporation, and compatibility with many industrial resins and formulations. Manufacturers select […]
Methylal Solvent: Uses and Properties
Methylal Solvent: Powerful Uses and Industrial Applications Methylal Solvent, also known as dimethoxymethane, is a highly volatile, flammable organic solvent used in selected chemical processing and specialty formulations. Its low boiling point and solvent properties make it worth evaluating for applications where rapid evaporation and compatibility with other formulation ingredients are important. For manufacturers, selecting […]
Best Industrial Solvent: Manufacturing Buyer’s Guide
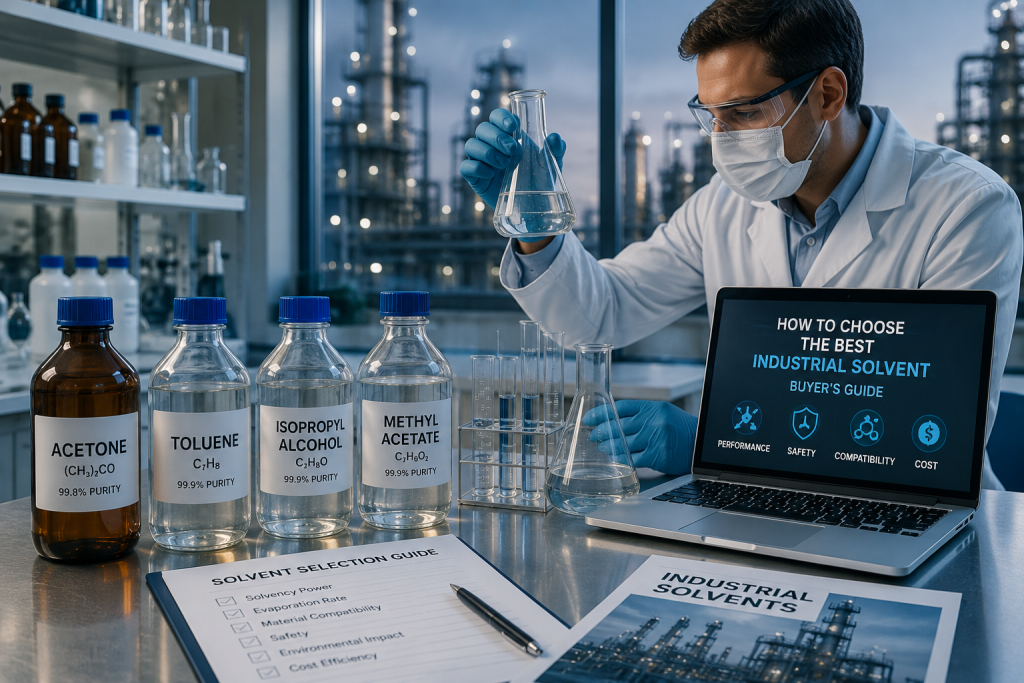
Selecting the best industrial solvent requires evaluating solvency, evaporation rate, material compatibility, purity, safety, and total operating cost. The right solvent helps manufacturers maintain product quality, improve processing efficiency, and reduce waste. However, the most suitable option depends on the formulation, equipment, and intended application. Manufacturers in paints and coatings, plastics, adhesives, printing, electronics, and […]