


Solvent Recovery Systems: 9 Powerful Benefits for Chemical Manufacturing
Solvent Recovery Systems: 12 Powerful Benefits for Chemical Industry Efficiency Introduction Solvent Recovery Systems are advanced industrial technologies designed to recover, purify, and reuse valuable solvents generated during chemical and manufacturing processes. Instead of treating used solvents as waste, these systems convert them into reusable raw materials, significantly improving efficiency, reducing operational costs, and supporting […]
Waterborne Acrylic Resins: Eco-Friendly Industrial Solutions
Waterborne Acrylic Resins: Eco-Friendly Industrial Solutions Waterborne acrylic resins are innovative polymers designed to provide high performance while minimizing environmental impact.Unlike solvent-based systems, waterborne resins utilize water as the primary carrier, reducing volatile organic compound (VOC) emissions and making industrial processes safer for workers and the environment.Their versatility allows usage in coatings,paints,adhesives,and various specialty applications. […]
7 Powerful Reasons Why Bio-Based Acetone Is the Future of Chemical Manufacturing
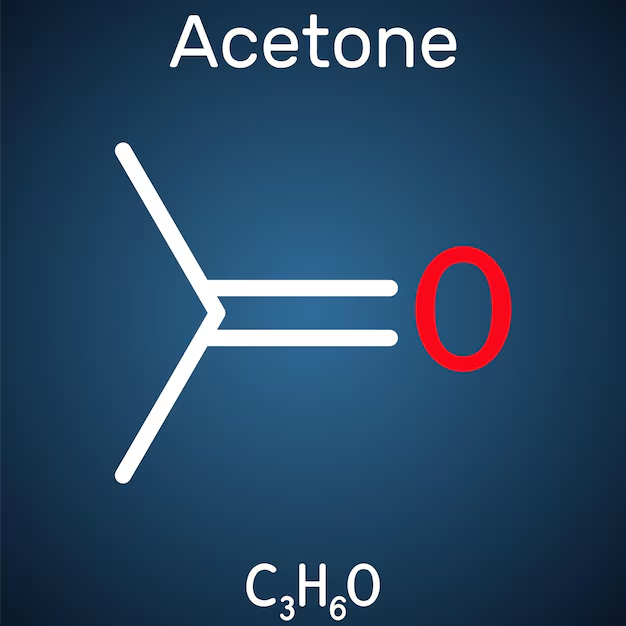
7 Powerful Reasons Why Bio-Based Acetone Is the Future of Chemical Manufacturing Bio-Based Acetone is rapidly emerging as a sustainable alternative to conventional petrochemical solvents in modern chemical manufacturing. Driven by stricter environmental regulations, rising demand for green solvents, and advancements in bio-refining technologies, this renewable form of acetone is reshaping industrial production strategies worldwide. […]
7 Benefits of Ethyl Lactate as a Green Solvent in Industrial Chemistry
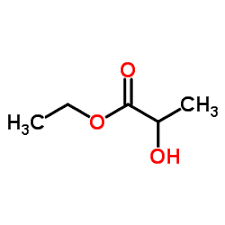
7 Benefits of Ethyl Lactate: Industrial Applications and Green Chemistry Industrial Ethyl Lactate Applications are expanding rapidly as industries adopt greener, safer solvents. Derived from renewable resources like corn and sugarcane, Ethyl Lactate is biodegradable and offers high performance while reducing environmental impact. Its properties make it essential in coatings, adhesives, pharmaceuticals, and sustainable chemical […]