


Solvents for Adhesives and Sealants: Uses
Solvents for Adhesives and Sealants in Industry Solvents for Adhesives and Sealants play an important role in industrial adhesive formulations by helping dissolve compatible resins, control viscosity, and regulate drying time. Choosing the right solvents for adhesives and sealants can improve application consistency, substrate compatibility, and production efficiency in packaging, automotive, construction, and footwear manufacturing. […]
Industrial Cleaning Solvents: Uses & Selection
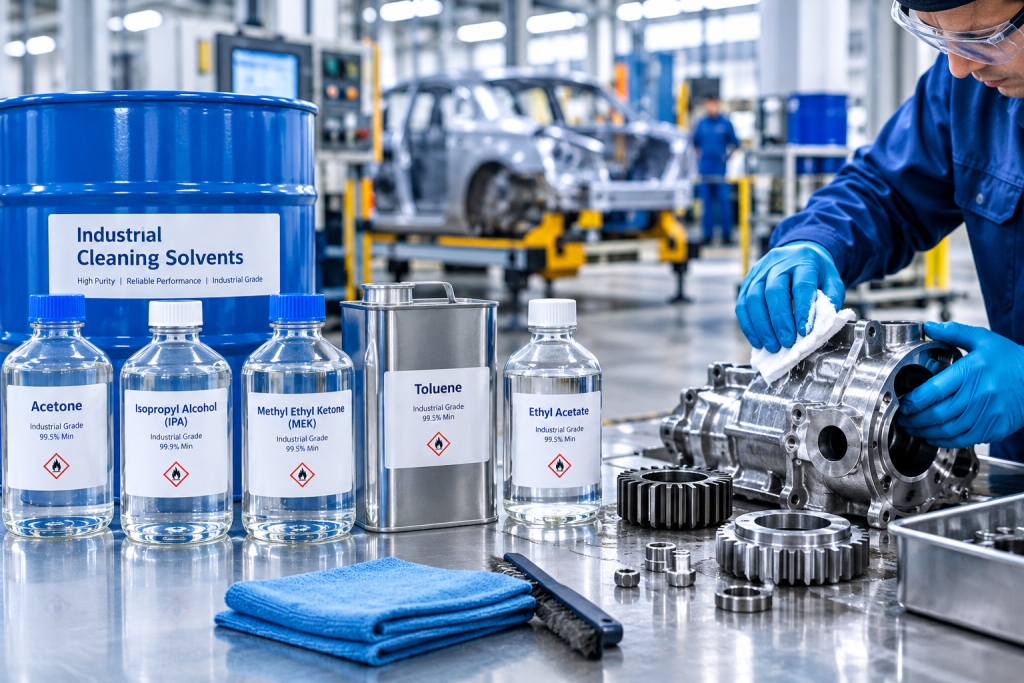
Industrial Cleaning Solvents: Uses and Selection Industrial Cleaning Solvents help manufacturers remove oil, grease, adhesive residues, uncured coatings, and other contaminants from machinery, metal components, and production surfaces. Selecting the right industrial cleaning solvent improves cleaning efficiency, prepares surfaces for subsequent processing, and helps protect sensitive materials from chemical damage. What Are Industrial Cleaning Solvents? […]
Industrial Solvents for Paints and Coatings
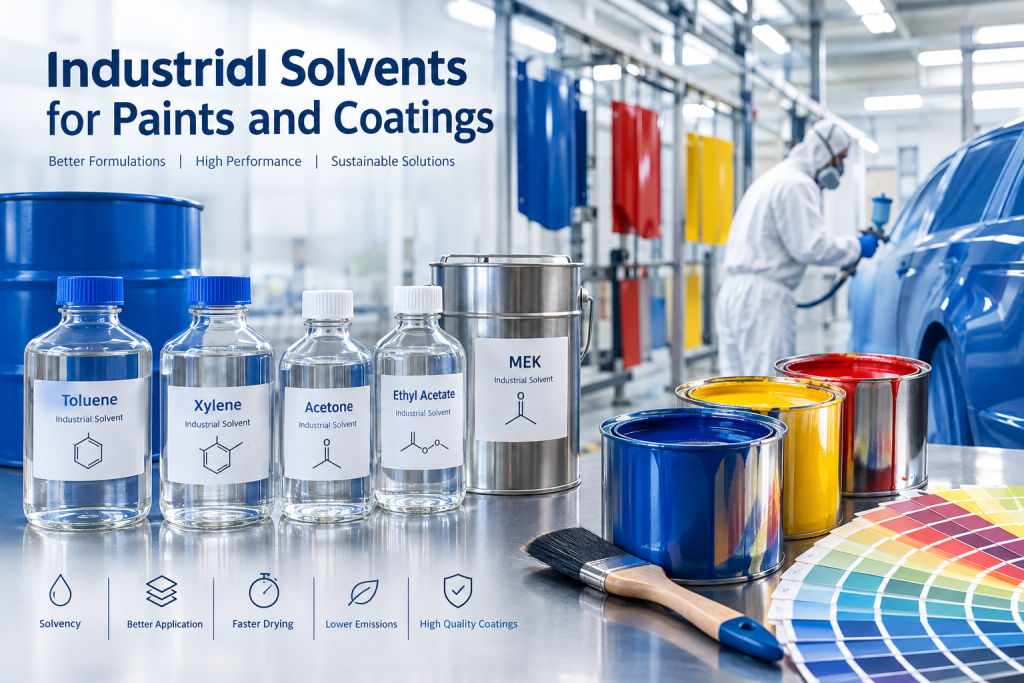
Paints and Coatings Industrial Solvents for Paints and Coatings: Uses and Selection Industrial Solvents for Paints and Coatings help manufacturers control resin compatibility, viscosity, flow, and drying behavior in solvent-based coating formulations. Selecting the right solvent system can improve application consistency, surface appearance, and production efficiency across automotive, metal finishing, furniture, machinery, and protective coating […]
Pharmaceutical Solvents: Uses and Selection
Pharmaceutical Solvents: Applications and Selection Pharmaceutical solvents play a vital role in drug manufacturing, active pharmaceutical ingredient (API) production, extraction, purification, crystallization, and equipment cleaning. Selecting suitable solvents helps pharmaceutical manufacturers maintain process consistency, control impurities, and meet the quality requirements of their intended applications. Common pharmaceutical solvents include ethanol, isopropyl alcohol, acetone, and ethyl […]
Low VOC Solvents: Uses and Industrial Benefits
Low VOC Solvents: Uses and Industrial Benefits Low VOC Solvents are used in industrial formulations designed to reduce volatile organic compound (VOC) emissions while meeting specific performance requirements. They are relevant to paints, coatings, adhesives, printing inks, cleaning products, and chemical manufacturing, where solvent selection affects formulation stability, application, drying, and emissions. Choosing suitable low […]
Bio-Based Solvents: Industrial Uses and Benefits
Bio-Based Solvents: Industrial Uses and Benefits Bio-based solvents are solvents produced partly or entirely from renewable biological resources, such as plant oils, sugars, and agricultural materials. These materials can provide alternatives to conventional petroleum-derived solvents in selected industrial applications. Understanding their properties, limitations, and compatibility helps manufacturers choose suitable solvents for coatings, adhesives, printing, and […]
Methanol Uses: Industrial Applications & Benefits
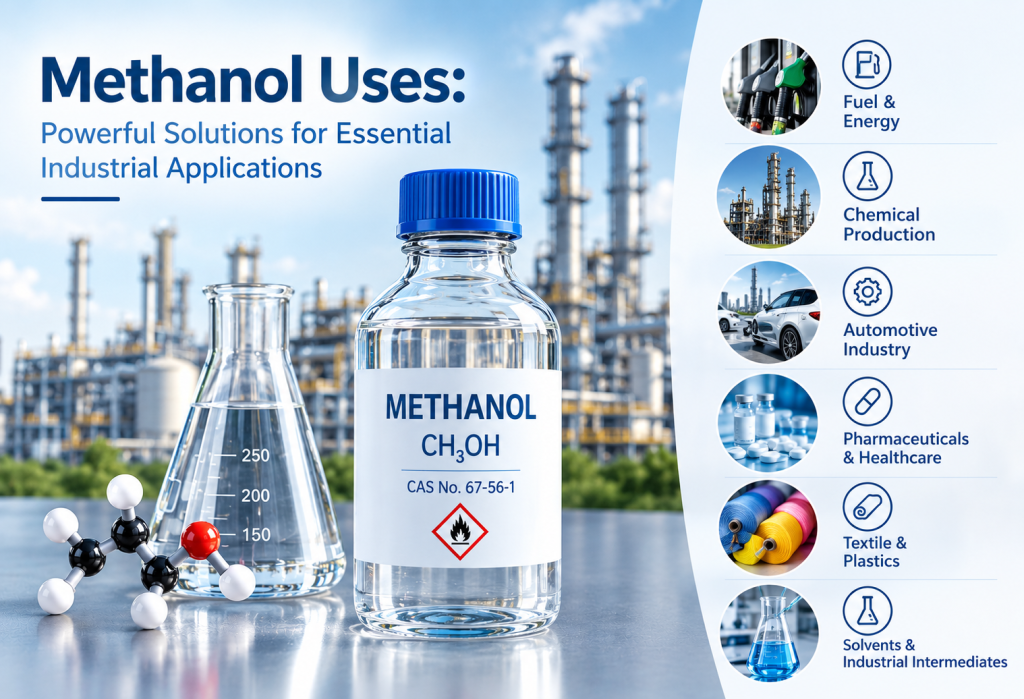
Methanol Uses: Industrial Applications and Benefits Methanol Uses span chemical manufacturing, fuel production, laboratory analysis, and selected industrial processes. Methanol (CH₃OH), also known as methyl alcohol, is a colorless, volatile, and highly flammable liquid used mainly as a chemical feedstock and, in specific applications, as a solvent. Understanding methanol properties, industrial applications, and safety requirements […]
Isopropyl Alcohol Uses: Industrial Applications
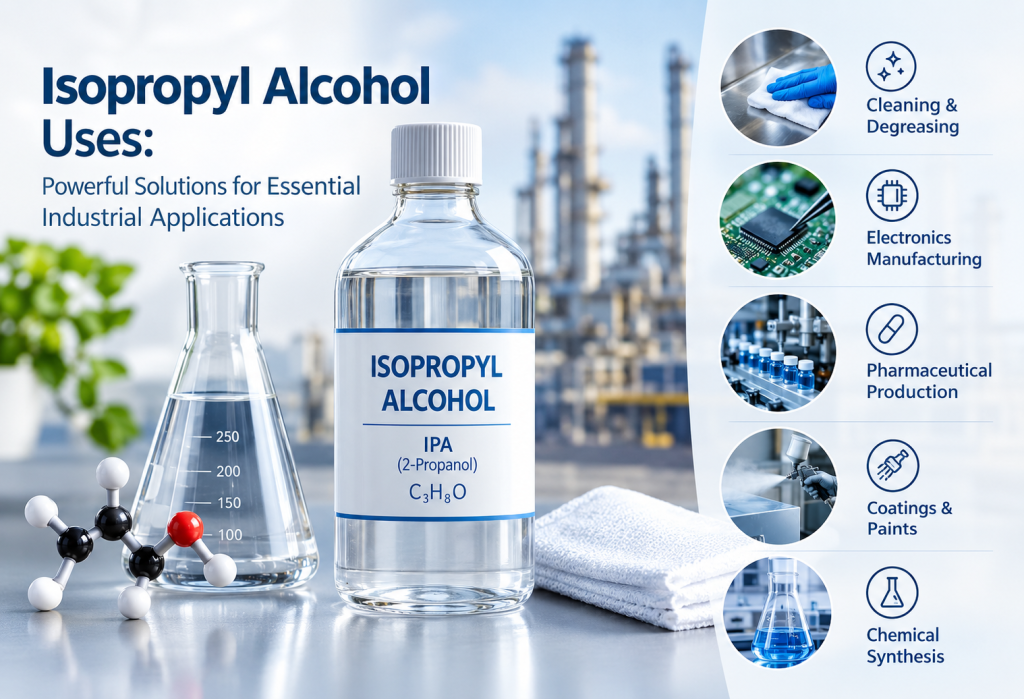
Isopropyl Alcohol Uses: Industrial Applications Isopropyl Alcohol Uses include electronics cleaning, pharmaceutical processing, laboratory analysis, printing, coatings, and industrial manufacturing. Isopropyl alcohol (IPA), also known as isopropanol or 2-propanol, is a colorless, volatile, and flammable liquid valued for its solvent properties and relatively rapid evaporation. With a chemical formula of C₃H₈O and CAS number 67-63-0, […]
Ethyl Acetate Uses: Industrial Applications
Ethyl Acetate Uses: Industrial Applications Ethyl Acetate Uses include paints and coatings, adhesives, printing inks, pharmaceutical processing, and selected food and cosmetic applications. Ethyl acetate is a volatile organic ester solvent valued for its ability to dissolve many resins and organic compounds and for its relatively rapid evaporation. With the chemical formula C₄H₈O₂ and CAS […]
Xylene Uses: Industrial Applications and Benefits
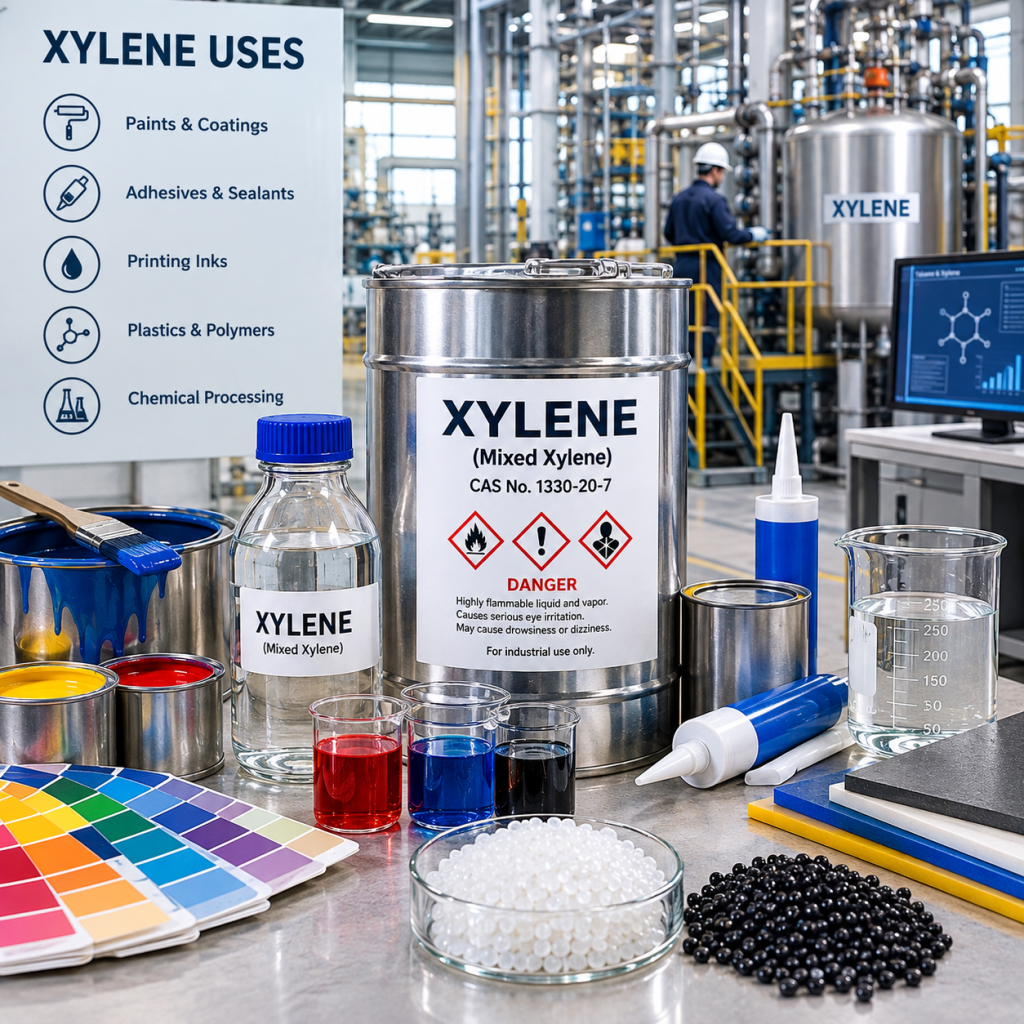
Xylene Uses: Industrial Applications and Benefits Xylene Uses include industrial solvent applications and petrochemical manufacturing. Xylene is an aromatic hydrocarbon available as three isomers—ortho-xylene, meta-xylene, and para-xylene—as well as commercial mixtures known as mixed xylene. Manufacturers use the appropriate grade according to its solvency, isomer composition, purity, and process requirements. From paints and coatings to […]