


Low VOC Solvents: Uses and Industrial Benefits
Low VOC Solvents: Uses and Industrial Benefits Low VOC Solvents are used in industrial formulations designed to reduce volatile organic compound (VOC) emissions while meeting specific performance requirements. They are relevant to paints, coatings, adhesives, printing inks, cleaning products, and chemical manufacturing, where solvent selection affects formulation stability, application, drying, and emissions. Choosing suitable low […]
Sustainable Epoxy Resins
Sustainable Epoxy Resins for Industrial Applications Sustainable Epoxy Resins are an innovative solution for industrial polymers, combining high performance with environmental responsibility. These eco-friendly resins reduce reliance on fossil-based raw materials while maintaining exceptional mechanical and chemical properties. Asad Shimi provides a wide range of sustainable epoxy resins and technical guidance to support manufacturers in […]
Biodegradable Polymers: Innovations in Sustainable Materials for Industry
Biodegradable Polymers: Innovations in Sustainable Materials for Industry Biodegradable Polymers are transforming the materials industry by providing sustainable and eco-friendly alternatives to conventional plastics. Derived from renewable resources or designed to decompose naturally, these green polymers reduce environmental impact while maintaining high performance. Industries worldwide are adopting these sustainable polymers for packaging, coatings, medical devices, […]
Propylene Carbonate: A Safe and Versatile Industrial Solvent
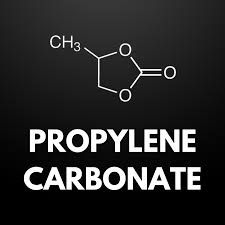
Propylene Carbonate: A Safe and Versatile Industrial Solvent Propylene Carbonate is widely recognized as a safe and versatile industrial solvent with growing importance in modern chemical manufacturing. Due to its excellent solvency power, low toxicity, and high boiling point, it has become a preferred choice across multiple industries including batteries, coatings, pharmaceuticals, and specialty chemicals. […]