


Solvent Recovery Systems: 9 Powerful Benefits for Chemical Manufacturing
Solvent Recovery Systems: 12 Powerful Benefits for Chemical Industry Efficiency Introduction Solvent Recovery Systems are advanced industrial technologies designed to recover, purify, and reuse valuable solvents generated during chemical and manufacturing processes. Instead of treating used solvents as waste, these systems convert them into reusable raw materials, significantly improving efficiency, reducing operational costs, and supporting […]
Propylene Carbonate: A Safe and Versatile Industrial Solvent
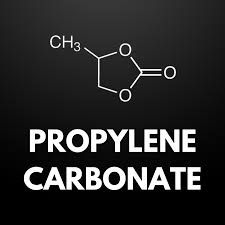
Propylene Carbonate: A Safe and Versatile Industrial Solvent Propylene Carbonate is widely recognized as a safe and versatile industrial solvent with growing importance in modern chemical manufacturing. Due to its excellent solvency power, low toxicity, and high boiling point, it has become a preferred choice across multiple industries including batteries, coatings, pharmaceuticals, and specialty chemicals. […]
7 Powerful Reasons Why Bio-Based Acetone Is the Future of Chemical Manufacturing
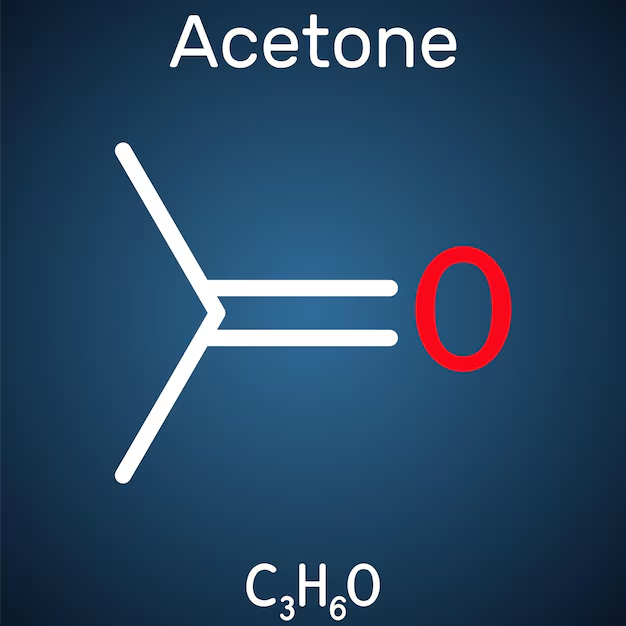
7 Powerful Reasons Why Bio-Based Acetone Is the Future of Chemical Manufacturing Bio-Based Acetone is rapidly emerging as a sustainable alternative to conventional petrochemical solvents in modern chemical manufacturing. Driven by stricter environmental regulations, rising demand for green solvents, and advancements in bio-refining technologies, this renewable form of acetone is reshaping industrial production strategies worldwide. […]