


Table of Contents
- Acetone Specifications and Physical Properties
- What Are the Main Acetone Uses in Industry?
- 1. Acetone Uses in Industrial Cleaning
- 2. Acetone Uses in Paints, Coatings, and Printing Inks
- 3. Acetone Uses in Adhesives, Resins, and Polymer Processing
- 4. Acetone Uses in Chemical Manufacturing
- Why Is Acetone Used as a Fast-Evaporating Solvent?
- Acetone vs. MEK: Which Solvent Is Better?
- How to Select the Right Acetone Grade
- Acetone Safety, Handling, and Storage
- Conclusion: Choosing Acetone for Industrial Applications
- What are the main acetone uses in industry?
- Why is acetone used for industrial cleaning?
- Is acetone soluble in water?
- What is the difference between acetone and MEK?
- Is acetone flammable?
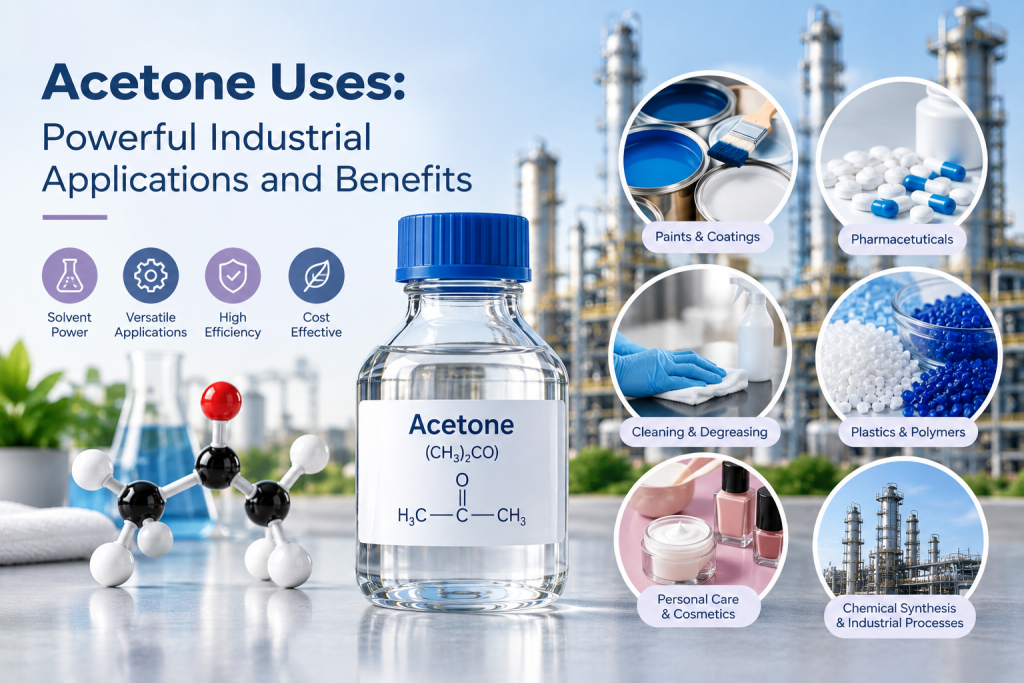
Acetone uses cover a wide range of industrial applications, including surface cleaning, paint and coating production, adhesive manufacturing, and chemical processing. These acetone uses make this fast-evaporating solvent valuable for manufacturers that need effective dissolving performance, efficient cleaning, and reliable processing results.
Acetone, also known as propanone, is a clear, colorless liquid that dissolves many organic substances and mixes completely with water. Its volatility and solvent properties make it suitable for specific manufacturing processes, although the correct grade depends on purity, material compatibility, and application requirements.
Acetone Specifications and Physical Properties
| Property | Typical Value |
|---|---|
| Chemical Name | Acetone |
| Synonyms | Propanone, 2-Propanone, Dimethyl Ketone |
| Chemical Formula | C₃H₆O |
| CAS Number | 67-64-1 |
| EC Number | 200-662-2 |
| Molecular Weight | 58.08 g/mol |
| Appearance | Clear, colorless liquid |
| Melting Point | Approximately −94.7°C |
| Boiling Point | Approximately 56.1°C at 1 atm |
| Flash Point | Approximately −20°C; method-dependent |
| Density | Approximately 0.79 g/cm³ at 20°C |
| Viscosity | Approximately 0.32 mPa·s at 20°C |
| Water Solubility | Miscible with water |
These are typical reference values. Actual specifications may vary slightly depending on test methods and product grade. Buyers should check the supplier’s Technical Data Sheet (TDS) and Certificate of Analysis (CoA) before selecting acetone for a specific process.
What Are the Main Acetone Uses in Industry?
The main acetone uses are associated with its solvent strength, low boiling point, and rapid evaporation. Manufacturers use it in applications where dissolving performance and drying speed are important. However, its suitability must be evaluated against the material, formulation, and operating conditions.
1. Acetone Uses in Industrial Cleaning
One of the most common acetone uses is industrial cleaning. Acetone can remove selected oils, grease, adhesive residues, and other organic contaminants from compatible surfaces. It is used in equipment maintenance, component preparation, and cleaning before certain coating or bonding operations.
Its rapid evaporation can help reduce drying time after cleaning. Nevertheless, acetone may damage certain plastics, elastomers, painted surfaces, and protective finishes. Manufacturers should test compatibility on a small area before introducing acetone into a cleaning process.
2. Acetone Uses in Paints, Coatings, and Printing Inks
Acetone is used in selected paint, coating, and printing ink formulations as a solvent or formulation component. It can help dissolve compatible ingredients and influence viscosity, application behavior, and drying characteristics.
These acetone uses are particularly relevant when a formulation requires fast solvent evaporation. Formulators must still consider resin compatibility, working time, film formation, substrate sensitivity, and applicable emissions requirements. The ideal solvent blend depends on the chemistry of the finished product.
3. Acetone Uses in Adhesives, Resins, and Polymer Processing
In adhesive and resin manufacturing, acetone can dissolve compatible materials, support selected processing steps, and clean production equipment. It may also be used for surface preparation when the substrate can tolerate the solvent.
Not every adhesive or polymer is compatible with acetone. Before using it, manufacturers should assess the possibility of swelling, cracking, surface damage, reduced adhesion, or other performance problems. Testing the complete process is more reliable than selecting a solvent based on its name alone.
4. Acetone Uses in Chemical Manufacturing
Acetone serves as a solvent and processing aid in selected chemical synthesis, extraction, and purification operations. Its ability to dissolve many organic compounds makes it useful in processes where a volatile solvent is required.
Purity requirements vary between applications. Technical-grade acetone may suit some industrial processes, while laboratory, pharmaceutical, or regulated applications can require tighter specifications and documented quality controls. The selected grade must meet the requirements of the intended use.
Why Is Acetone Used as a Fast-Evaporating Solvent?
A key reason behind many acetone uses is its low boiling point of approximately 56.1°C at atmospheric pressure. This property allows acetone to evaporate rapidly under typical conditions. Its ability to dissolve many organic substances and mix with water further expands its usefulness in selected cleaning and formulation tasks.
Rapid evaporation can shorten drying time, but it can also increase vapor concentrations and reduce the time available for coating or bonding operations. Manufacturers should balance solvent performance with ventilation, fire protection, exposure controls, and final product quality.
Acetone vs. MEK: Which Solvent Is Better?
Acetone and methyl ethyl ketone (MEK) are both ketone solvents, but they have different evaporation profiles and formulation behavior. Acetone generally evaporates faster, while MEK has a higher boiling point and may provide a longer working time in some applications.
The better choice depends on the resin system, required solvency, drying speed, substrate compatibility, cost, and workplace requirements. Manufacturers should compare both solvents under actual operating conditions rather than assuming that one is suitable for every application.
For more technical reading, explore our industrial chemical articles and related solvent information.
How to Select the Right Acetone Grade
Choosing the correct grade helps ensure that acetone performs as expected in the intended process. Different acetone uses may require different purity levels, impurity limits, and documentation.
- Purity: Select a grade that meets the requirements of the formulation or manufacturing process.
- Impurity limits: Review water content, residue, and other relevant quality parameters.
- Batch consistency: Request a current TDS and CoA to verify product specifications.
- Packaging: Use compatible, tightly sealed containers designed for flammable liquids.
- Supply reliability: Confirm product availability, documentation, and delivery requirements.
Matching the grade to the application can improve process consistency and help prevent defects caused by unsuitable specifications. To review available chemical products, visit the Aasad Chimie products page. For product specifications, availability, or a quotation, contact the Aasad Chimie team.
Acetone Safety, Handling, and Storage
Although acetone is useful in many industrial processes, it is highly flammable. Its vapor can form ignitable mixtures with air, so workplaces must keep it away from heat, sparks, open flames, and other ignition sources.
Use acetone in a suitably ventilated area and store it in appropriate, tightly closed containers. Select protective equipment according to the task and exposure assessment. Follow the supplier’s Safety Data Sheet (SDS), workplace procedures, and applicable regulations for handling, spill response, fire protection, and waste disposal.
Rapid evaporation does not eliminate the need for exposure controls. Workers should avoid breathing concentrated vapors and prevent unnecessary contact with skin and eyes.
Conclusion: Choosing Acetone for Industrial Applications
Acetone uses include industrial cleaning, surface preparation, selected coating and ink formulations, adhesive and resin processing, and chemical manufacturing. Its solvent strength and rapid evaporation can support efficient production, but the correct grade depends on the formulation, substrate, and required quality standards.
Before purchasing, verify technical specifications, review material compatibility, and follow appropriate safety procedures. For additional chemical information, consult the PubChem acetone reference and the NIOSH Pocket Guide to Chemical Hazards.
What are the main acetone uses in industry?
The main acetone uses include industrial cleaning, surface preparation, selected paints and coatings, printing inks, adhesive production, resin processing, and chemical manufacturing.
Why is acetone used for industrial cleaning?
Acetone dissolves many organic contaminants and evaporates quickly. Its suitability depends on the type of contamination, surface compatibility, and workplace safety requirements.
Is acetone soluble in water?
Yes. Acetone is completely miscible with water. However, its compatibility with other formulation ingredients must be evaluated separately.
What is the difference between acetone and MEK?
Acetone generally evaporates faster than MEK. The appropriate solvent depends on the required solvency, drying time, formulation, and material compatibility.
Is acetone flammable?
Yes. Acetone is highly flammable and must be handled with adequate ventilation, ignition-source control, suitable containers, and the precautions specified in its Safety Data Sheet.